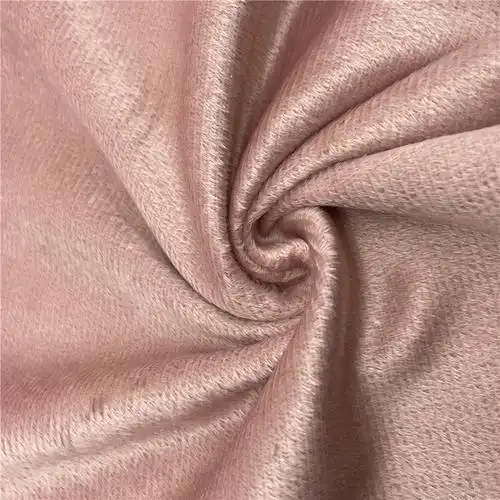
Flocking creates a rich, velvet-like texture that transforms ordinary garments into premium, tactile design statements. From high-density suede-like prints to soft-touch branding accents, flocking adds visual depth and warmth to modern apparel. However, one persistent challenge haunts garment production and customer satisfaction: flock shedding. When short textile fibers detach easily during wear or laundering, the premium aesthetic degrades rapidly.
Eliminating fiber fall-off requires moving beyond trial-and-error manufacturing. The key to long-lasting flocking lies in mastering the dynamic interaction between two core parameters: adhesive chemical mechanics and electrostatic field strength. Achieving the ideal balance between glue viscosity, layer thickness, and electrical field intensity ensures maximum fiber penetration, vertical alignment, and permanent anchor strength.
Understanding the Physics of Electrostatic Flocking
To eliminate shedding, it is essential to understand how short precision-cut fibers (typically nylon, rayon, or polyester) move during the application process.
When a high-voltage electrostatic generator creates a direct current field (typically between 30 kV and 90 kV) between the dosing hopper and the grounded garment surface, tiny fibers receive a charge. Driven by electrostatic forces, these charged fibers align vertically along the electric field lines and accelerate downwards at high velocity.
Upon impact, the fibers pierce into the wet adhesive layer pre-printed onto the fabric surface. If the adhesive is too dry or hard, fibers bounce off or sit loosely on top. If the electrostatic field is too weak, fibers land at flat, slanted angles—drastically reducing the contact surface area and weakening mechanical anchoring.
Parameter 1: The Chemistry and Dynamics of the Adhesive Layer
The adhesive layer serves as the foundation matrix. Managing its wet-state properties determines how effectively fiber ends are locked into place.
1. Viscosity and Rheology Control
Adhesive viscosity controls penetration resistance. If the glue is overly fluid, it soaks deep into the fabric base, leaving insufficient adhesive volume on the surface to hold the fibers. Conversely, high viscosity prevents incoming fibers from sinking deep enough into the glue bead. A balanced viscosity (typically 15,000 to 25,000 cPs depending on fiber denier) allows rapid fiber penetration without fabric strike-through.
2. Wet Layer Thickness Rule
A core rule in high-durability flocking is matching adhesive wet film thickness to fiber length. As an industry baseline, the wet adhesive thickness should equal 10% to 15% of total fiber length.
- For 0.8 mm (800 microns) nylon flock, the wet adhesive layer must measure between 80 and 120 microns.
- Anything thinner leads to shallow fiber anchoring and premature shedding.
- Anything thicker causes a stiff hand-feel, glue bleeding, and extended drying times.
3. Polymer Curing and Open Time
The adhesive must remain wet and open throughout the flocking cycle. Waterborne polyurethane adhesives and cross-linked acrylic emulsions offer superior elasticity and wash durability. Adding cross-linking agents prior to printing enhances water resistance and wash stability, ensuring the bond holds even after repeated machine laundering.
Parameter 2: Fine-Tuning the Electrostatic Field
The electrostatic field supplies the kinetic energy required to propel fibers deep into the adhesive bed with high velocity and vertical precision.
1. Field Strength and Voltage Alignment
Electric field strength ($E$) is governed by the applied voltage ($V$) divided by the distance ($d$) between the charging electrode and the garment:
$$E = \frac{V}{d}$$
For optimal fiber momentum and alignment, aim for an electric field strength of 3.0 to 5.0 kV/cm.
- Electrode Distance: Maintain a consistent clearance of 8 to 12 cm between the dosing screen and the substrate.
- Applied Voltage: Set DC voltage between 40 kV and 60 kV depending on ambient humidity and fiber thickness.
2. Charge Density and Fiber Velocity
Insufficient field voltage results in low fiber velocity. Fibers hit the wet glue sluggishly, producing a loose, tilted pile that sheds easily under friction. Excessive voltage, on the other hand, creates spark discharges, field distortion, and fiber repulsion (“hedgehog effect”), where fibers push away from one another and form uneven clumps.
The Golden Ratio: Adhesive & Electrostatic Balance Matrix
Shed-proof flocking is achieved when wet adhesive thickness and electrostatic voltage work in complete alignment:
| Fiber Length & Material | Target Wet Adhesive Thickness | Recommended Voltage | Distance | Optimal Viscosity Range |
| 0.5 mm Rayon / Nylon | 60 – 80 microns | 35 – 45 kV | 8 – 10 cm | 12,000 – 18,000 cPs |
| 0.8 mm Nylon | 80 – 120 microns | 45 – 55 kV | 10 – 12 cm | 15,000 – 22,000 cPs |
| 1.0 mm Polyester | 120 – 150 microns | 55 – 65 kV | 10 – 12 cm | 18,000 – 25,000 cPs |
Critical Environmental Controls & Quality Testing
Even calibrated equipment requires proper atmospheric control to prevent electrostatic dissipation:
- Relative Humidity (RH) & Temperature: Maintain workplace humidity at 55% – 65% and ambient temperature at 20°C – 25°C. Low humidity causes static charge loss and fiber flyaway, while excessive moisture slows adhesive open time.
- Substrate Grounding: Ensure the printing platen or conveyor belt is fully grounded. Static accumulation on the garment repels incoming fibers, drastically lowering flock density.
- Durability Verification: Evaluate flock adhesion using a Martindale rub tester and standard 40°C wash cycles (testing for at least 25 wash cycles). Perform a cross-hatch tape test after full curing to confirm interfacial bond strength.
Building Premium Quality into Textile Craftsmanship
By treating flocking as a precise science—balancing electric field energy with wet glue film dynamics—apparel creators can eliminate fiber shedding completely. This calibration transforms soft-touch flocking from a high-maintenance accent into a durable, luxury feature built to survive years of wear and washing.